1. What Is Injection Molding?
Injection molding is one of the most widely used manufacturing processes for producing plastic parts at medium to high volumes. It is commonly used for electronic housings, automotive components, medical products, consumer goods, and industrial parts.
Its main advantages are high production efficiency, good repeatability, complex geometry capability, and low unit cost at scale.
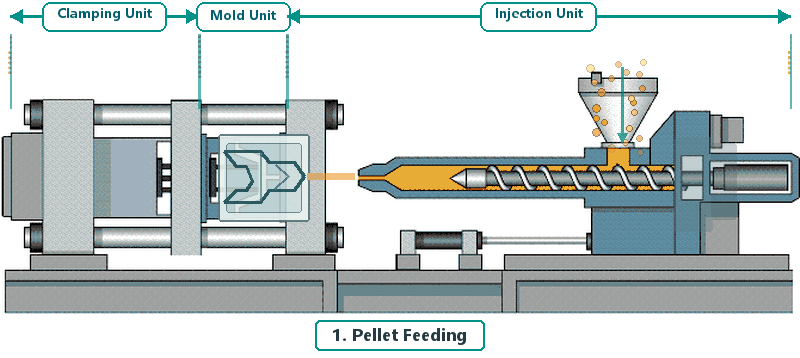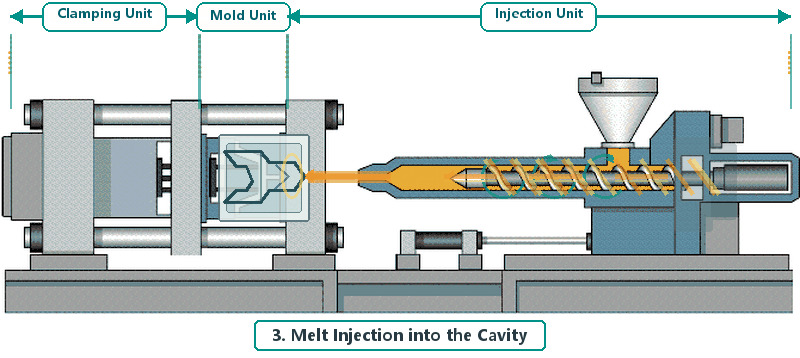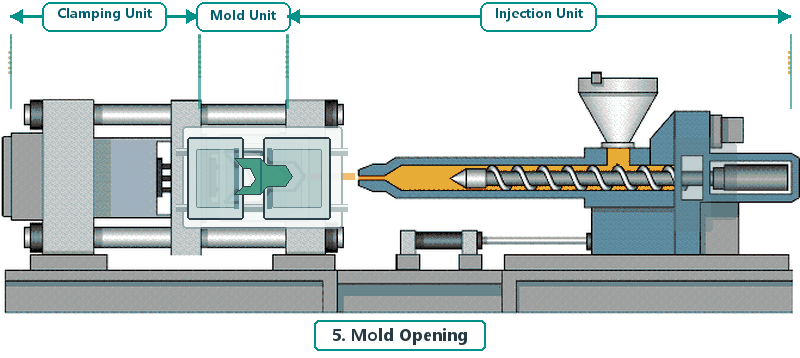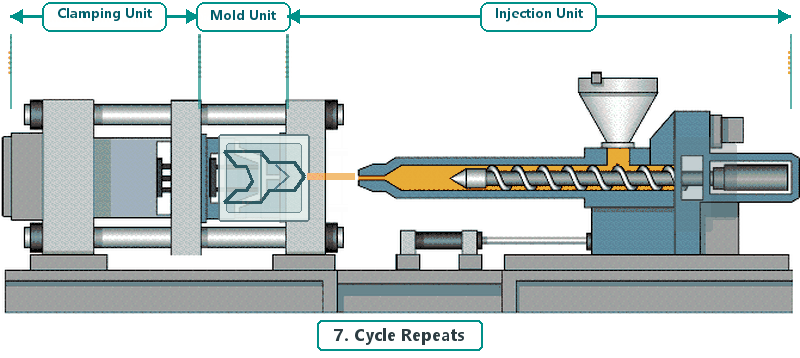
Injection molding is a manufacturing process in which plastic pellets are melted, injected into a closed mold cavity under pressure, cooled, and then ejected as a finished part. A typical molding cycle includes:
Material Feeding → Melting → Injection → Packing/Holding → Cooling → Mold Opening → Ejection
Once the mold and process parameters are stable, the process can repeatedly produce large quantities of parts with consistent dimensions and appearance.
2. How Injection Molding Works
Plastic pellets enter the injection molding machine through a hopper and are transported through a heated barrel by a rotating screw. The material is gradually melted and mixed before the screw moves forward and injects the molten plastic into the mold cavity.
After filling, holding pressure is applied to compensate for material shrinkage. The part is then cooled until sufficiently solid before the mold opens and the part is ejected. Key process parameters include: Melt temperature, Mold temperature, Injection pressure, Injection speed, Holding pressure, Cooling time.
Even small changes in these parameters can affect part dimensions, appearance, and stability.
3. Common Injection Molding Materials
Material selection should consider strength, temperature resistance, chemical resistance, shrinkage, appearance, and cost.
| Material | Main Characteristics | Typical Applications |
|---|---|---|
| ABS | Tough, easy to process, good surface finish | Electronic housings, appliances |
| PP | Lightweight, flexible, chemical resistant | Containers, automotive parts |
| PC | High impact resistance, heat resistant | Covers, structural components |
| PA / Nylon | High strength and wear resistance | Gears, brackets, mechanical parts |
| POM | Low friction, good dimensional stability | Precision gears, moving components |
| PMMA | High transparency | Light covers, transparent components |
| TPU / TPE | Flexible and elastic | Seals, grips, overmolding |
| PC+ABS | Good strength and processability | Automotive and electronic housings |
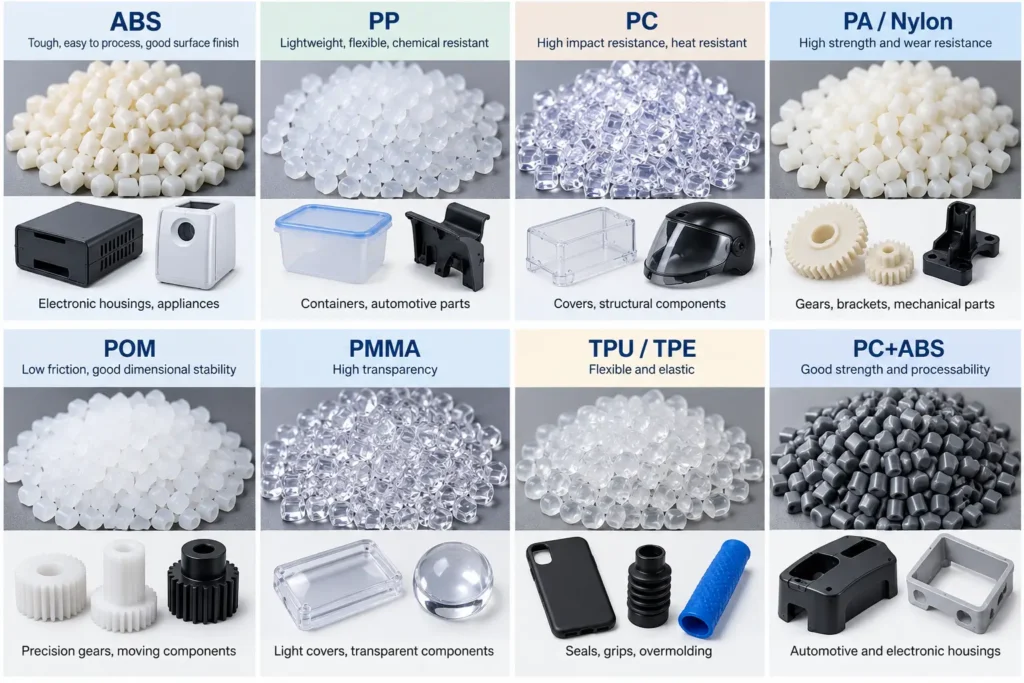
There is no single “best” injection molding plastic. The material should always be selected according to the product’s operating environment and functional requirements.
4. Common Injection Molding Defects
Injection molding defects are often caused by a combination of part design, mold design, material behavior, and process parameters.
| Defect | Typical Causes |
| Sink Marks | Thick sections, insufficient holding pressure, uneven cooling |
| Short Shot | Low injection pressure, poor venting, low melt temperature |
| Flash | Excessive pressure, mold wear, insufficient clamping force |
| Weld Lines | Multiple flow fronts meeting, low material or mold temperature |
| Warpage | Uneven wall thickness, unbalanced cooling, uneven shrinkage |
| Burn Marks | Trapped air, poor venting, excessive injection speed |
| Flow Marks | Improper flow speed, low mold temperature, poor gate design |
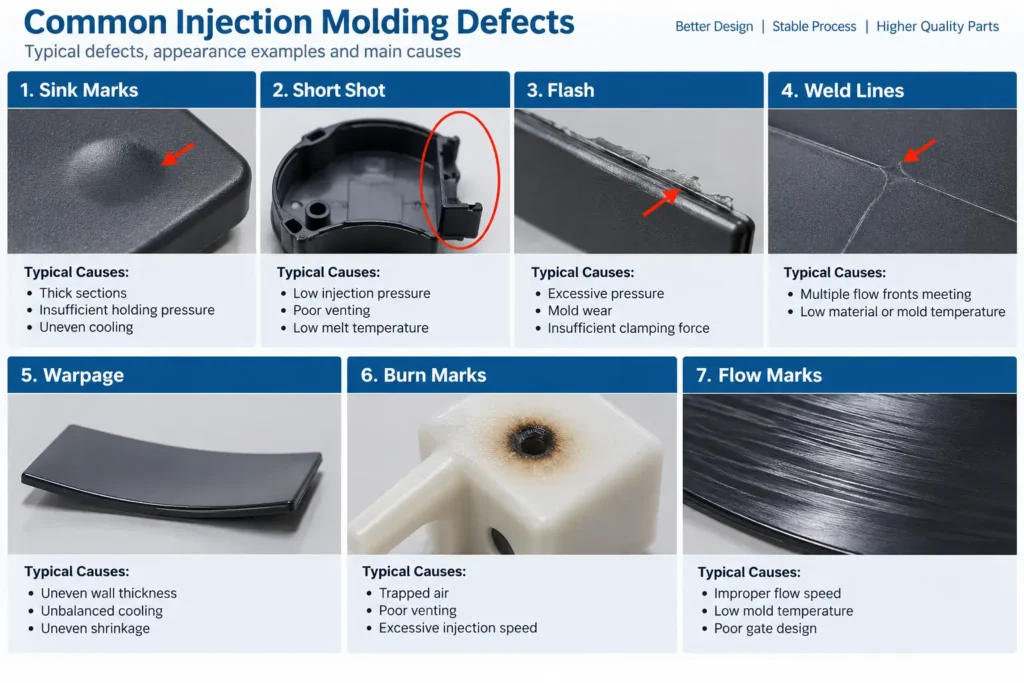
Many defects cannot be completely solved by adjusting machine parameters alone. Part geometry and mold design should also be reviewed during root-cause analysis.
5. Injection Molding Tolerance
Injection molded plastic parts naturally shrink during cooling. Unlike CNC machining, where dimensions are directly machined from a relatively stable workpiece, molded plastic dimensions can be affected by:
- Material shrinkage
- Mold temperature
- Cooling rate
- Part geometry
- Gate location
- Process stability
For this reason, tighter tolerances generally require tighter control of both mold construction and molding conditions. Critical dimensions should be clearly identified during the design stage rather than applying unnecessarily tight tolerances to every feature. This helps reduce mold complexity, inspection cost, and production risk.
Conclusion
Injection molding is a highly efficient process for producing plastic parts at scale, but stable production depends on the combination of material selection, mold design, process control, and dimensional requirements.
For engineers and buyers, considering manufacturability early can significantly reduce mold modifications, quality problems, and overall project cost.
FAQ
Injection molding is a manufacturing process that melts plastic material and injects it into a mold cavity under pressure. After cooling, the finished plastic part is ejected from the mold.
Common injection molding materials include ABS, PP, PC, Nylon (PA), POM, PMMA, TPU, TPE, and PC+ABS. Material selection depends on strength, temperature resistance, appearance, chemical resistance, and cost.
Injection molding tolerance depends on the material, part size, geometry, mold accuracy, and process control. Critical dimensions normally require tighter mold and molding-process control than general dimensions.
Common defects include sink marks, short shots, flash, weld lines, warpage, burn marks, and flow marks. These problems can be related to part design, mold design, material, or molding parameters.
Plastic contracts as it cools from molten material into a solid part. The amount of shrinkage varies depending on the plastic material, wall thickness, mold temperature, cooling conditions, and part geometry.
Defects can be reduced through proper DFM, material selection, gate and mold design, cooling control, and stable molding parameters. For many problems, changing machine settings alone is not enough.